


Controlling the Heat: How to Stop Thermal Drift in Gear Manufacturing
A common frustration on any busy shop floor is the “afternoon drift.” At the start of the shift, your CNC Gear Hobbing machine cuts perfect parts that easily pass inspection. But a few hours later, without any changes to the program or the tools, the inspection room starts reporting mid-shift gear profile errors and lead angle issues.
The operator did not make a mistake, and the cutting tool is not broken. The real problem is thermal drift in CNC machining.
When a machine runs continuously, it creates a lot of heat. This heat causes the machine’s metal frame, the spindle, and the workpiece to expand slightly. In gear manufacturing, where you are working with micron-level tolerances, even the smallest amount of metal expansion will shift your cutting alignment and scrap the part.
Relying on operators to constantly adjust offsets during their shift to chase these changing dimensions is stressful and leads to mistakes. To get true, stable production, you need a mix of good daily habits and smart machine design. Here is a practical guide to controlling heat on the shop floor.
1. Where Does the Heat Come From?
To stop thermal drift, you first need to know where the heat is coming from. During the gear hobbing process, heat comes from three main sources:
- Cutting Friction: Cutting metal at high speeds creates extreme friction. Ideally, most of this heat goes into the metal chips. However, if those hot chips pile up inside the machine, they act like a heater, transferring that heat directly into the machine bed and warping its shape.
- Machine Components: The spindle motors, bearings, and hydraulic systems work hard during continuous production. Running these parts at high speeds for hours generates internal heat that slowly warms up the entire machine structure.
- Shop Floor Temperature: Many manufacturing facilities are not temperature-controlled. The temperature difference between a cool morning and a hot afternoon causes the machine frame to naturally expand and contract as the day goes on.
2. Practical Steps for Operators to Control Heat
Operators cannot control the weather outside, but they can control how the machine handles heat inside. Following a few simple daily rules makes a big difference.
- Always Run a Warm-Up Cycle: Never start cutting precision gears on a “cold” machine. Operators should run the spindle and move the axes for 15 to 20 minutes before loading the first part. This brings the machine up to its normal operating temperature, meaning it has already finished expanding before the cutting begins.
- Keep the Chips Moving: Hot chips will ruin your accuracy if they sit inside the machine. Operators must make sure the chip conveyor is always running and clear away any chip pile-ups near the worktable or tailstock.
- Maintain the Coolant: A good gear hobbing coolant system carries heat away from the cutting zone. However, if the coolant mixture (Brix level) is incorrect, it loses its ability to cool the part properly. Operators must check and maintain the coolant concentration every single day.
3. The Machine’s Role: How Nimble Machines Solves the Problem
Good operator habits are important, but they are not enough if the machine itself cannot handle the heat. To truly beat thermal drift, you need a machine built with smart cooling technology.
This is exactly how Nimble Machines designs the VAJRA Series. These machines are built with built-in thermal management features to stop mid-shift gear profile errors before they happen:
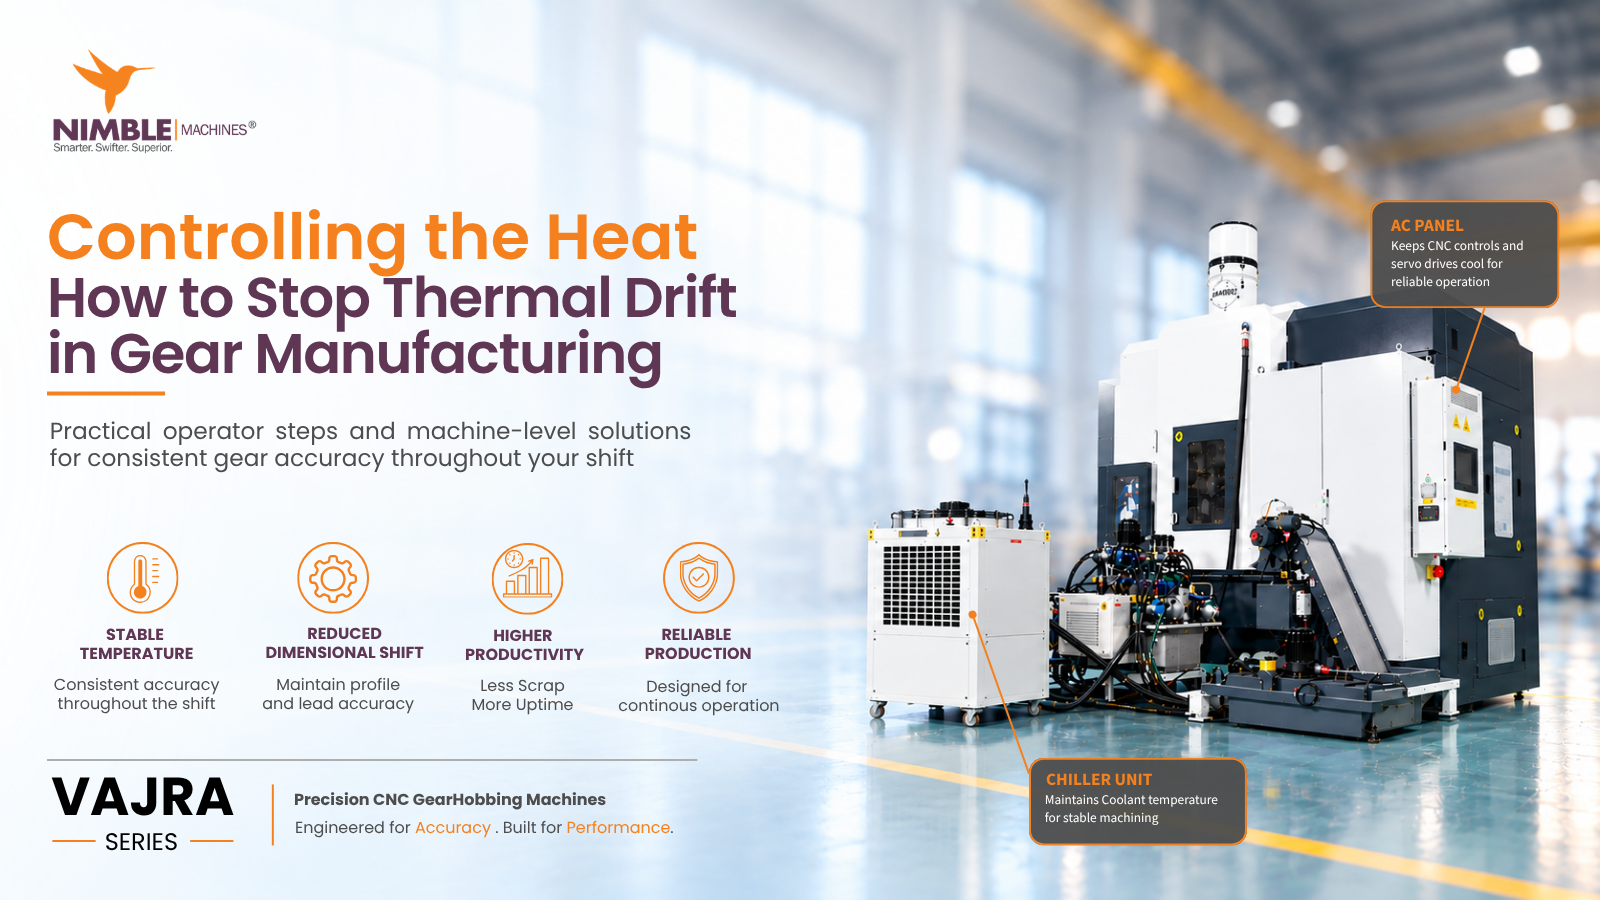
- Active Coolant Chillers: A standard coolant system just pumps the same fluid around, and it gets hotter as the day goes on. Nimble Machines prevents this by integrating an active Chiller Unit into their gear hobbing coolant system. This chiller keeps the cutting oil at one exact, cool temperature all day long, stopping heat from soaking into the machine.
- Air-Conditioned Electrical Panels: Heat is bad for metal, but it is also bad for electronics. Nimble Machines puts dedicated AC units on their electrical cabinets. Keeping the CNC controls and servo drives cool prevents the electrical glitches and lag that can cause machining errors.
- UCRIDE® Composite Base: The VAJRA series uses a special UCRIDE® composite material inside the critical parts of the machine base. This material acts as a thermal shield. It blocks heat from traveling through the machine column, keeping the structure straight and accurate even under heavy workloads.
- High-Speed Dry Hobbing: For the ultimate way to avoid coolant heat issues, the VAJRA Series is built for dry hobbing. Using special carbide tools, the machine cuts metal so fast that all the heat goes directly into the chips, not the part. The hot chips drop onto the conveyor and are carried away instantly, completely removing the heat from the cutting area.
By combining well-trained operators with a thermally stable CNC Gear Hobbing machine like the VAJRA 130R, plant managers can finally stop worrying about afternoon dimensional changes and keep their production perfectly on target.
Frequently Asked Questions
Thermal drift happens when a machine’s metal parts expand because of heat. This heat comes from the friction of the cutting tool, the motors running inside the machine, and changes in the room temperature. As the machine gets hotter and expands, the cutting tool shifts slightly, which pushes the gear out of its required tolerance.
A strong coolant system pulls heat away from the gear and the cutting tool. By using an active coolant chiller—like those provided by Nimble Machines—the cutting oil is kept at a constant, cool temperature. This stops the machine and the workpiece from heating up and changing size during a long production run.
If your parts are changing size later in the day, you are dealing with thermal drift. As the machine runs for hours and the shop floor gets warmer in the afternoon, the machine’s cast-iron frame absorbs that heat and expands. If your machine does not have a coolant chiller or a thermally stable bed, this expansion will ruin your gear profiles and lead angles.
